Piegādes termiņš visā Lietuvā: 5-7 darba dienas.
Piegādes cena uz norādīto adresi: 3 eiro



Apraksts
Trumpai apie prekę
Prekė: Suvirinimo aparatas Sherman DIGITIG pulse AC/DC 225GD MIX. Kategorija: Inverteriniai suvirinimo aparatai.
- Gamintojas: Sherman
- Modelis: AC/DC 225GD MIX
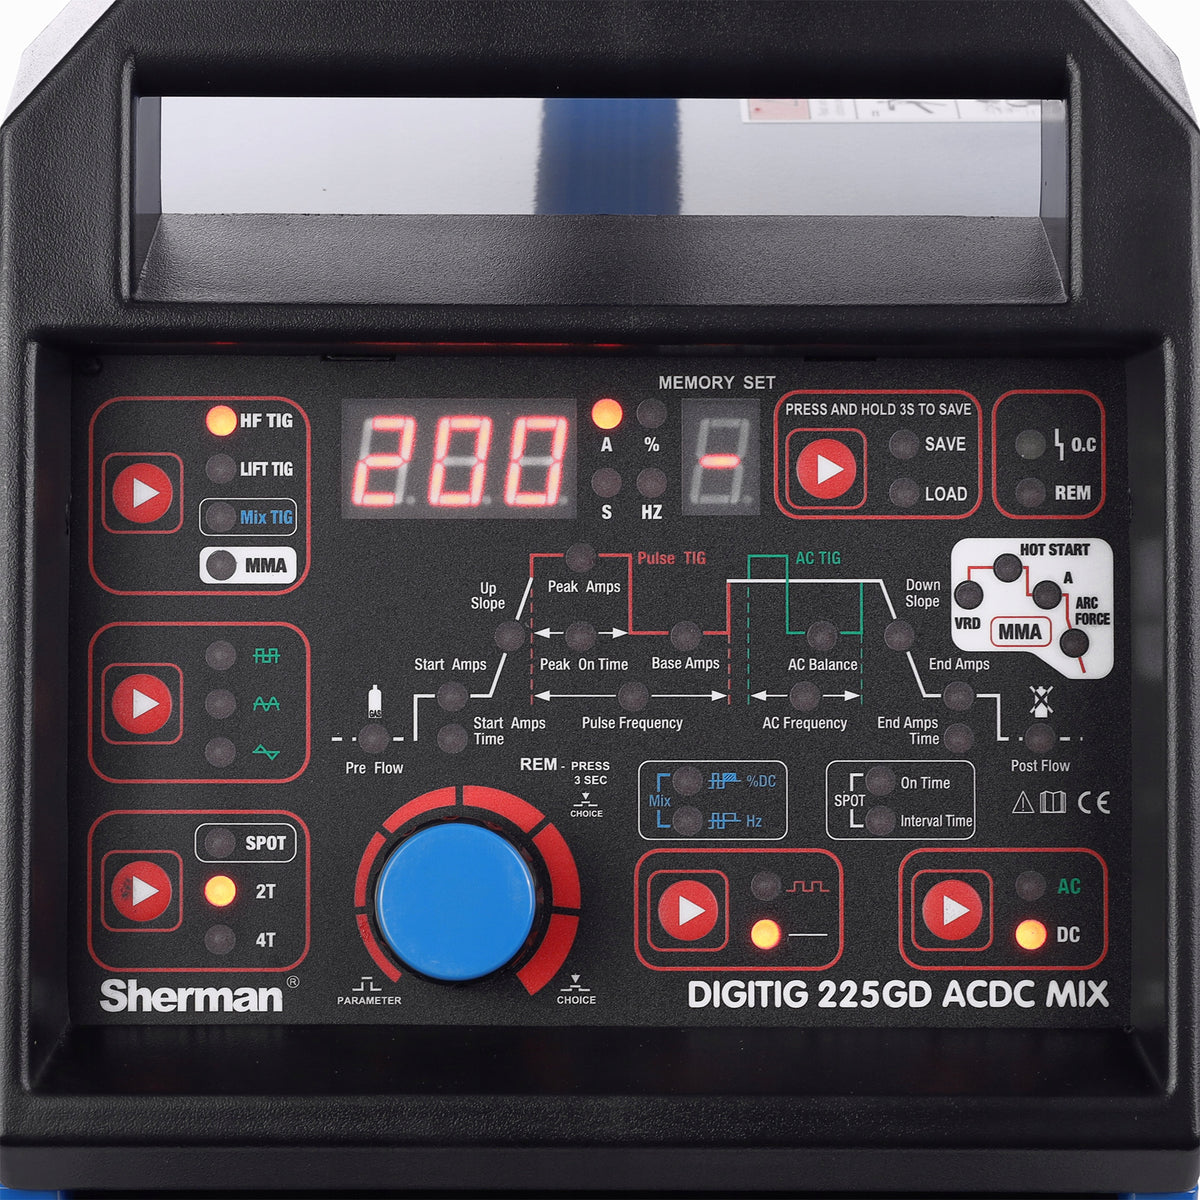
DIGITIG 225GD AC/DC MIX is a professional-grade digital inverter welding machine designed for welding with TIG AC/DC, TIG MIX and MMA methods. The device was made in IGBT technology and equipped with digital microprocessor control MCU, which allows precise setting of welding parameters, arc characteristics, pulse and AC operation.
The welding machine allows welding of steel, stainless steel, aluminum and non-ferrous metals. Thanks to the AC/DC MIX function, the device combines the advantages of direct and alternating current, ensuring a stable arc, good melting and effective cleaning of surfaces during welding of aluminum and its alloys.
✅ The most important features of the device
- Welding with TIG HF, TIG Lift, TIG MIX and MMA methods.
- Support for constant DC, alternating AC and mixed AC/DC MIX current.
- IGBT inverter technology for high efficiency and stability.
- Digital control of welding parameters using an MCU microcontroller.
- Possibility of welding aluminum, stainless steel, carbon steel and non-ferrous metals.
- Non-contact arc TIG HF and TIG Lift arc ignition by rubbing.
- TIG pulse adjustment: frequency, pulse width and base current.
- AC parameters adjustment: AC frequency, AC balance and waveform.
- MIX TIG function for mixed current AC/DC welding.
- Handle operating modes: 2T, 4T and spot welding SPOT.
- MMA features: VRD, Hot Start and Arc Force.
- Memory 10 sets of settings welding parameters.
- Fan Stop function limiting fan operation in the absence of full load.
- Thermal protection against overheating.
- Possibility of remote control.
✅ Application
The DIGITIG 225GD AC/DC MIX welding machine is suitable for professional locksmith, production, service, automotive workshops and assembly works. Thanks to the AC, DC and MIX modes, the device is suitable for welding steel, stainless steel, aluminum and non-ferrous metal elements.
The device can be used both for precise welding of thin materials using the TIG method, as well as for repair or construction work using electrodes wrapped in MMA mode.
✅ Methods of welding
TIG HF – tungsten electrode welding in an inert gas shield with non-contact arc ignition using an ionizer. This solution reduces the risk of contamination of the tungsten electrode and the welded material, because the electrode does not have to touch the surface of the element.
TIG Lift – TIG welding with arc ignition by rubbing. This mode does not generate high-frequency pulses, so it is useful in environments sensitive to interference, e.g. near electronics, CNC controllers or in car workshops.
TIG MIX – mixed current welding, combining DC and AC direct current. This feature allows for a stable, concentrated arc, deeper melting, and effective surface cleaning. It works particularly well when welding aluminum and its alloys.
MMA – welding with a wrapped electrode. The mode is designed for assembly, repair and construction work, where versatility and the ability to work with different types of electrodes are important.
✅ AC/DC MIX function
The AC/DC MIX mode enables alternating use of direct and alternating current during TIG welding. Increasing the share of DC current allows for a more stable and concentrated arc, greater melting, narrower weld and better control over the welding lake. A greater proportion of AC current provides a wider arc, more effective surface cleaning and shallower melting.
MIX frequency adjustment allows you to adjust the nature of the arc work to the type of material and the expected quality of the weld. Higher frequency affects more stable arc, deeper penetration, narrower weld and reduced chipping.
✅ AC waveform adjustment
The device allows you to choose the waveform of the AC current, which allows you to adjust the arc characteristics to the type of material and thickness of the element.
- Rectangular wave – a universal waveform, most often used for welding various materials. It provides more heat in the welding zone and deeper melting.
- Sine wave – classic operating characteristics, similar to transformer welding machines. Suitable for users who prefer traditional arch operation.
- Triangular wave – recommended especially for thin materials, where it is important to limit the amount of heat introduced into the welded element.
✅ TIG Functions
- Pre Flow – a pre-outflow of gas before arcing, providing a shield for the tungsten electrode and the place where welding begins.
- Start Amps – initial current facilitating arcing and control of the beginning of the weld.
- Start Amps Time – duration of the initial current.
- Up Slope – the time of current build-up from the initial value to the welding current.
- Peak Amps – welding current or peak current when working with pulse.
- Peak On Time – pulse width, affecting the amount of heat and depth of melting.
- Base Amps – base current, i.e. the lower pulse value when welding with a pulse.
- Pulse Frequency – pulse frequency that regulates the transitions between peak and base current.
- AC Frequency – AC frequency, especially important for welding aluminium.
- AC Balance – AC balance regulating the ratio of positive and negative phases, affecting surface cleaning, weld width and melting depth.
- Down Slope – the time of current drop, allowing you to control the end of the weld.
- End Amps – crater current that allows filling the end of the weld.
- End Amps Time – duration of crater current.
- Post Flow – gas flow after arc extinction, protecting the cooling weld and tungsten electrode from oxidation.
- SPOT On Time – adjustable spot welding time.
- SPOT Interval Time – adjustable interval between spot welding cycles.
✅ MMA Functions
VRD – a function that reduces voltage in the unloaded state. Increases work safety by reducing the risk of electric shock. The full voltage value is restored immediately before the arc is ignited.
Hot Start – a hot start function that temporarily raises the current during arc ignition. It facilitates the start of welding and reduces the risk of sticking the electrode to the material.
Arc Force – arc dynamics adjustment. Increasing the value causes deeper melting and facilitates welding with a short arc, while lower settings give a softer arc and a smaller depth of melting.
✅ Handle operating modes
2T – two-bar mode. Welding is carried out with the handle button pressed. Release of the button completes the welding process.
4T – four-bar mode. After pressing and releasing the handle button, welding continues without having to hold the button. Pressing the button again begins the welding process.
SPOT – spot welding mode with adjustable welding time and intervals between subsequent points.
✅ Settings memory
The welder has memory of the last used parameters and the ability to save 10 complete sets of settings. This feature makes it easy to quickly return to proven configurations for specific materials, component thicknesses or repetitive welding jobs.
✅ Cooling and protection
The device is equipped with the Fan Stop function, which turns off the fan after welding and cooling the device. The fan restarts under load. This solution reduces noise, reduces dust suction inside the welding machine and improves work comfort.
The welder also has thermal protection. In case of overheating, the device automatically disconnects the welding current, the O.C. light turns on, and the “Err” message appears on the display. When the temperature is lowered, the protection resets automatically.
✅ Technical data of welding machine:
- Power supply: AC 230 V ±10%, 50 Hz
- Maximum power consumption: MMA: 6,6 kVA / TIG: 4,2 kVA
- Rated welding current / duty cycle: MMA: 180 A / 60%; TIG: 200 A / 60%
- Nominal voltage without load: 23 V VRD / 59 V
- Maximum power consumption: MMA: 36,5 A / TIG: 26,8 A
- Network security: 25 A
- Degree of protection: IP21
- Dimensions: 455 x 195 x 415 mm
- Mass without accessories: 18,5 kg
✅ Parameter adjustment ranges:
- Arc Force: 0 – 100 A
- Hot Start: 0 – 50 A
- Gas flow: 0,1 – 3 s
- Gas flow: 0 – 15 s
- Power build-up: 0 – 15 s
- Power drop: 0 – 25 s
- Initial current: 5 – 200 A
- Initial current duration: 0 – 10 s
- MMA welding current: 20 – 180 A
- TIG DC welding current: 5 – 200 A
- TIG AC welding current: 10 – 200 A
- Base current: 5 – 95% welding current
- Crater current: 10 – 200 A
- Crater current duration: 0,1 – 10 s
- Pulse frequency: 0,5 – 200 Hz
- Pulse width: 10 – 90%
- AC frequency: 20 – 200 Hz
- AC Balance: 20 – 80%
- Mixed current frequency MIX: 0,1 – 10 Hz
- Mixed current balance MIX: 10 – 90%
- Spot welding time: 0,1 – 10 s
- Break time during spot welding: 0 – 10 s
✅ TIG handle parameters
- Handle type: T-26
- Maximum current capacity: 200 A
- Gas flow: 10 – 20 l/min
- Arc ignition: Non-contact HF
- Handle length: 4 m
✅ Working conditions
- Ambient temperature range: -10°C to +40°C.
- Relative humidity: up to 80%.
- Atmospheric pressure: 860 – 1060 hPa.
- Working height: up to 1000 m above sea level.
- Permissible fluctuations in supply voltage: up to ±10%.
- The device is designed to work in closed rooms; the degree of protection IP21 does not allow work in the rain.
✅ Set equipment
- Welding source DIGITIG 225GD AC/DC MIX – 1 pc.
- TIG handle – 1 pc.
- Bulk cable with tick clamp – 1 pc.
- User manual – 1 pc.
- Packaging – 1 pc.
✅ Summary
DIGITIG 225GD AC/DC MIX is an advanced TIG AC/DC welding machine with mixed current function, designed for users requiring wide parameter adjustment and high quality welds. The device combines TIG welding precision, MMA functionality, digital control, settings memory and extensive regulation of AC current, pulse and MIX mode.
With a current range of up to 200 A in TIG, aluminium welding capabilities and arc stability support functions, this model is suitable for workshop, manufacturing and service applications.
Specifications
| Group | Name | Value |
|---|---|---|
| Parametry | Condition | new |
| Parametry | Invoice | With a VAT invoice |
| Parametry | Brand | Sherman |
| Parametry | Manufacturer code | 7813322 |
| Parametry | EAN (GTIN) | 5903686620522 |
| Parametry | Packaging status | original |
| Parametry | Model | AC/DC 225GD MIX |