Pristatymo terminas visoje Lietuvoje: 5-7 d.d.
Pristatymo kaina nurodytu adresu: Pristatymas nemokamas




Aprašymas
Trumpai apie prekę
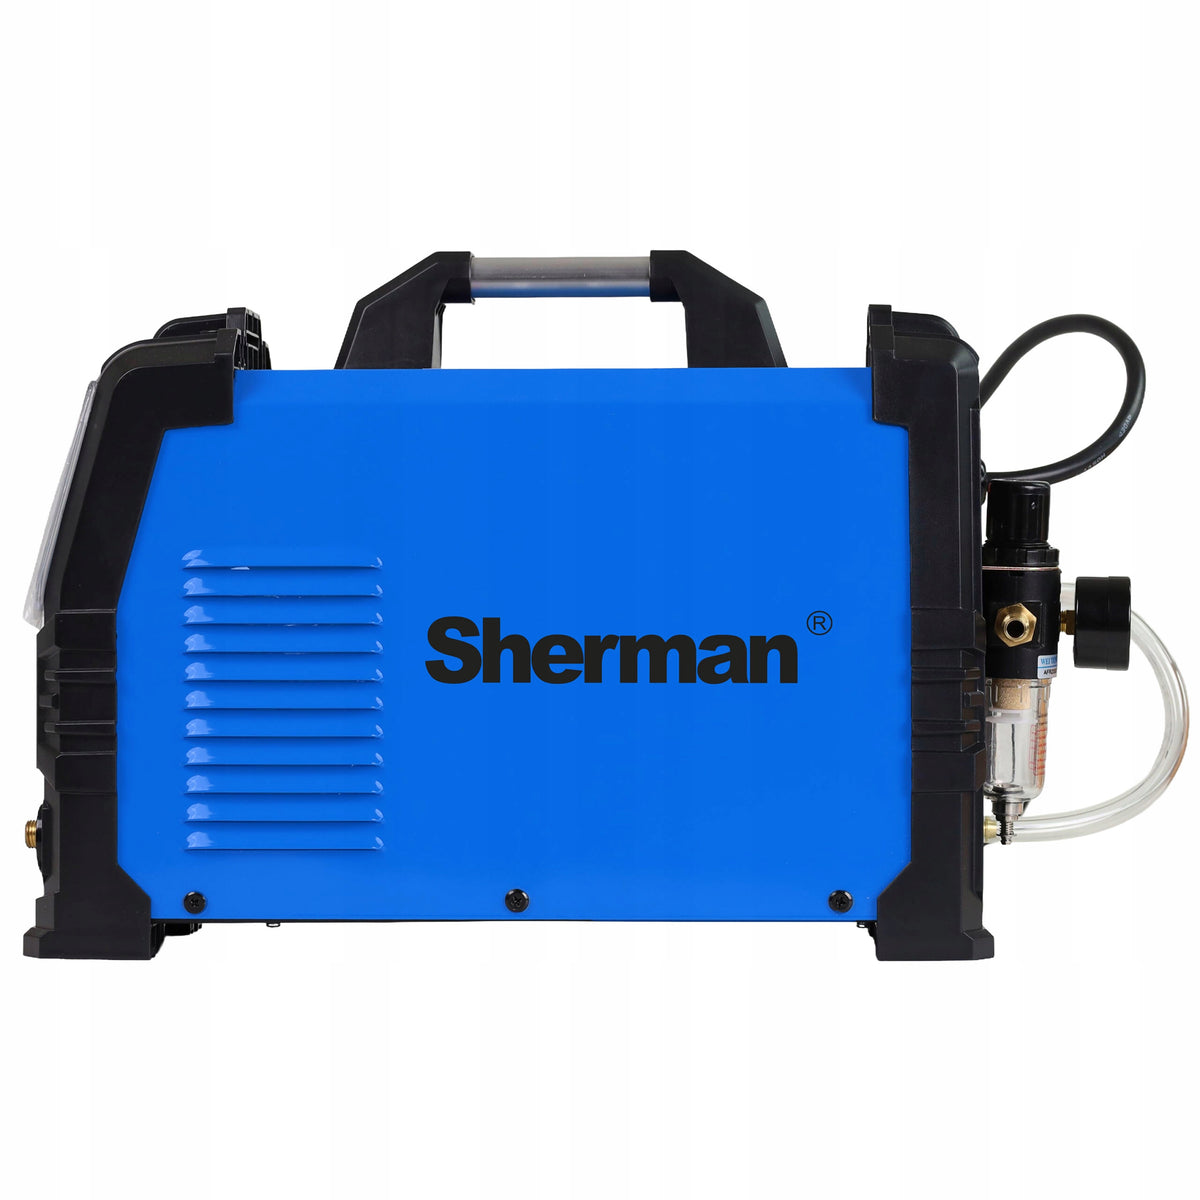
Prekė: Suvirinimo aparatas su plazmos pjaustytuvu Sherman DIGITIG 204 QUATTRO. Kategorija: Inverteriniai suvirinimo aparatai.
- Gamintojas: Sherman
- Modelis: DIGITIG 204 QUATTRO
SHERMAN DIGITIG 204 QUATTRO PLASMA
Manufacturer: Sherman | Welding methods: MMA, TIG HF DC, Cold Welding, Plasma cutting | Power supply: 230V | Welding current: 200A | Efficiency: 60% | Cutting current range: 15-50A | Max cutting thickness: 12mm
STANDARD EQUIPMENT:
- Sherman DIGITIG 204 QUATTRO welding machine with plasma cutter
- TIG-17 4m welding torch
- Plasma holder PT-31 4m
- Electrode cable
- Bulk cable
- Air preparation unit
Other accessories needed for full operation of the welding machine such as
- gas cylinder,
- welding wires
- visor, gloves
- Welding torch spare parts
The DIGITIG 204 QUATTRO welding machine is the latest generation device, made in IGBT technology and equipped with digital control.
It is used for manual welding using TIG DC method, MMA (wrapped electrode) of steel and non-ferrous metals with direct current with the possibility of using current pulsation. It also enables plasma cutting of steel, aluminum and copper sheets and elements.
Digital control allows full adjustment and control of welding parameters of arc and pulse characteristics. Thanks to the Fan Stop function, the noise level has been significantly reduced when the fan is turned off at low load.
In addition, it has HF, the ability to control in two-bar and four-bar mode, and a variant of spot welding, the so-called. cold welding (cold welding).
The welder is made in IGBT inverter technology, which allowed for a significant reduction of its weight and dimensions. Stable output parameters guarantee high quality weld.
Example applications: light industry, field renovation works, workshop work, automotive, silencer welding.
TECHNICAL DATA:
- Catalog number: 7812713
- Welding methods: MMA, TIG HF DC, Cold Welding, Plasma cutting
- Power supply voltage [V]: AC 230 50Hz
- Max. power consumption [A]: 30 A MMA: 29 A: TIG 21 A; CUT: 30 A
- Welding / cutting current MMA: 20-180 A; TIG: 10-200 A; CUT: 15 – 50 A
- Welding current [A]: MMA: 180 A / 25%; TIG:200A / 60%
- Maximum cutting thickness [mm]: 12
- Working cycle [%]: MMA: 180 A / 25%; TIG:200A / 60%
- Voltage in foreign state. [V]: MMA: 68 V, TIG: 68 V; CUT: 245 V
- Gas flow: 0 – 2 s
- Gas flow: 1 – 15 s
- Power build-up: 0 – 15 s
- Power drop: 0 – 15 s
- Initial current: 10 – 200 A
- Base current: 10 – 200 A
- Crater current: 10 – 200 A
- Pulse frequency: 0,5 - 200 Hz
- Pulse width: 10 – 90 %
- Welding time during spot welding: 0,01 – 2,5 s
- Break time during spot welding: 0,1 – 10 s
- Mass [kg]: 8,5
- Dimensions (D x SZ x W) [mm]: 430 x 170 x 310
IGBT TECHNOLOGY
Modern technology based on bipolar transistors with an isolated gate. It combines the ease of control of field transistors with high breakdown voltage and the speed of switching bipolar transistors. The use of IGBT technology has an impact on significantly extending the reliable operation of welding equipment.
DEGREE OF PROTECTION
IP23 means that the device is designed to work indoors and is not suitable for use in the rain.
PROTECTION AGAINST OVERHEATING
The IGBT module is protected from overheating by a protective installation that turns off the welding circuit of the device. After a few minutes, the welding machine is cooled to a temperature allowing it to be switched on again automatically.
WORK CYCLE
The work cycle is based on a 10-minute period. The 60% duty cycle means that a 4-minute break is required after 6 minutes of operation of the device. The 100% duty cycle means that the device can work continuously, without interruptions.
MMA
A method in which a wrapped electrode is used, consisting of a metal core covered with a sheath. The device allows welding with all types of electrodes, e.g. alkaline, cellulose, rutile or acidic.
VRD
The VRD function reduces the voltage in the unloaded state. The correct voltage value is restored only just before the arc is ignited. This minimizes the risk of electric shock, but in some cases it can make it difficult to light the arc.
TIG DC HF
In order to completely eliminate the possibility of contamination of the tungsten weld, it is recommended that the electrode does not touch the welded element; for this purpose, contactless arc ignition is used using high-frequency discharges generated by the built-in ionizer.
HF - NON-CONTACT ARC IGNITION
The device is equipped with an ionizer enabling contactless arc ignition.
2T/4T OPERATING MODE
2T - pressing the button in the handle of the handle turns on the ionizer and lights up the arc. Welding is carried out with the button pressed.
4T - pressing the button in the handle of the handle will turn on the ionizer and light up the arc then release the button and conduct welding with the button released. Pressing the button again will finish welding
INITIAL CURRENT
Current appearing in the circuit after pressing the button in the handle. The higher the initial current, the easier it is to light the arc.
However, when welding thin sheets, too high an initial current value can lead to sheet metal burning. In some welding modes, the current does not increase to heat the welded element.
TIME OF ELECTRICITY BUILD-UP
The time of current build-up of welding from the initial current to the set value of the welding current.
TIME OF CURRENT DROP
Welding current drop time from set to zero or crater current value.
TIME OF PRE-EXHAUST GAS
Time from pressing the button in the handle and opening the gas valve to the moment the arc ignites. Usually, it should be longer than 0,5 s to deliver shielding gas to the nozzle outlet of the burner to cover the welding start site and tungsten electrode.
GAS OUTFLOW TIME
Time from arc extinction to closing the gas valve to shield the solidifying welding lake from air and to cool the tungsten electrode. Too short outflow time can result in oxidation of the weld. When welding in TIG AC mode (alternating current), this time should be longer.
TIG DC
Allows TIG welding with DC current. This is required for welding non-ferrous metals.
TIG PULSE
The function affects the shape of the weld and the focus of the arc. Pulse welding also reduces the amount of heat supplied to the material and is applicable when welding thin materials.
PULSE FREQUENCY
Frequency with which the value of the current pulse changes between the welding current and the base current.
PULSE WIDTH
Pulse duration, allows you to adjust the depth of melting. The increase in width increases the depth of melting, reducing the amount of heat introduced into the material, reducing the risk of burning thinner sheets or smaller elements.
CRATER CURRENT
The current used in some welding modes when the arc is not extinguished immediately after the welding current drops. It allows you to fill the crater and the end of the weld.
COLD TIG
Point variety of TIG welding – so-called. cold welding for bonding thin elements, thanks to very low heat emission in the joining zone. It consists in cyclic short-term ignition and extinction of the arch.
- SPOT Pressing the switch in the handle of the handle will turn on the ionizer, light the arc for the time set by the COLD TIME parameter and extinguish the arc. Re-ignition of the arch requires releasing and pressing the button in the handle.
COLD TIME 0,01 – 2,5 p.
Welding time during spot welding (cold welding).
PAUSE TIME 0,1 – 10 seconds
Interruption time during spot welding (cold welding). Only for CPOT control mode.
Easy to use control panel allows precise and smooth adjustment of parameters. Digital display indicates the actual current during welding.
PLASMA
Function for cutting electrically conductive elements made of carbon and alloy steels, aluminium and its alloys, brass, copper, as well as cast iron
MAXIMUM CUTTING THICKNESS 12MM
The value of the maximum cutting thickness was determined under optimal cutting conditions of ordinary quality carbon steel. In order to select the right device, it is recommended to perform technological tests in real working conditions and on an example sample of material.
STRONG AND ROBUST CONSTRUCTION
The housing of the device is made of light and durable composites, resistant to all kinds of mechanical damage.
EASY TRANSPORT
Equipping the welding machine with a transport handle for convenience when changing jobs.
COOLING
The device has a cooling system with a fan which significantly increases its efficiency.
Specifications
| Group | Name | Value |
|---|---|---|
| Parametry | Condition | new |
| Parametry | Invoice | With a VAT invoice |
| Parametry | Brand | Sherman |
| Parametry | Power consumption | 5.8 kVA |
| Parametry | Supply voltage (V) | 230 |
| Parametry | Duty cycle time | 60% |
| Parametry | Maximum electrode diameter | 3.2 mm |
| Parametry | Device weight | 8.5 kg |
| Parametry | Welding range | 10–200 A |
| Parametry | Length of ground cable | 200 cm |
| Parametry | Welding cable length | 400 cm |
| Parametry | Product weight with unit packaging | 20 kg |
| Parametry | Manufacturer code | 7812713 |
| Parametry | EAN (GTIN) | 5903686618277 |
| Parametry | Model | DIGITIG 204 QUATTRO |
| Parametry | Welding methods | plasma cutting,MMA,TIG |
| Parametry | Additional features | infinitely adjustable welding current,LCD display |